
Freezing Food in Plastic Containers: Why -18 °C Decides the PP vs PET Question
A tub in a -18 °C freezer store carries load for its entire declared shelf life, commonly 6 to 18 months, with no rest period. Nothing about that load is passive. The wall is the only element taking it, and it takes it without interruption.
Two variables decide whether the tub survives: the polymer grade, and the wall specification — nominal and minimum thickness, rib geometry, taper, corner radius. Neither is decisive alone, which is how tubs marketed as freezer-safe plastic containers still crack at the base corner after two pallet movements.
The Four Concurrent Stressors at -18 °C
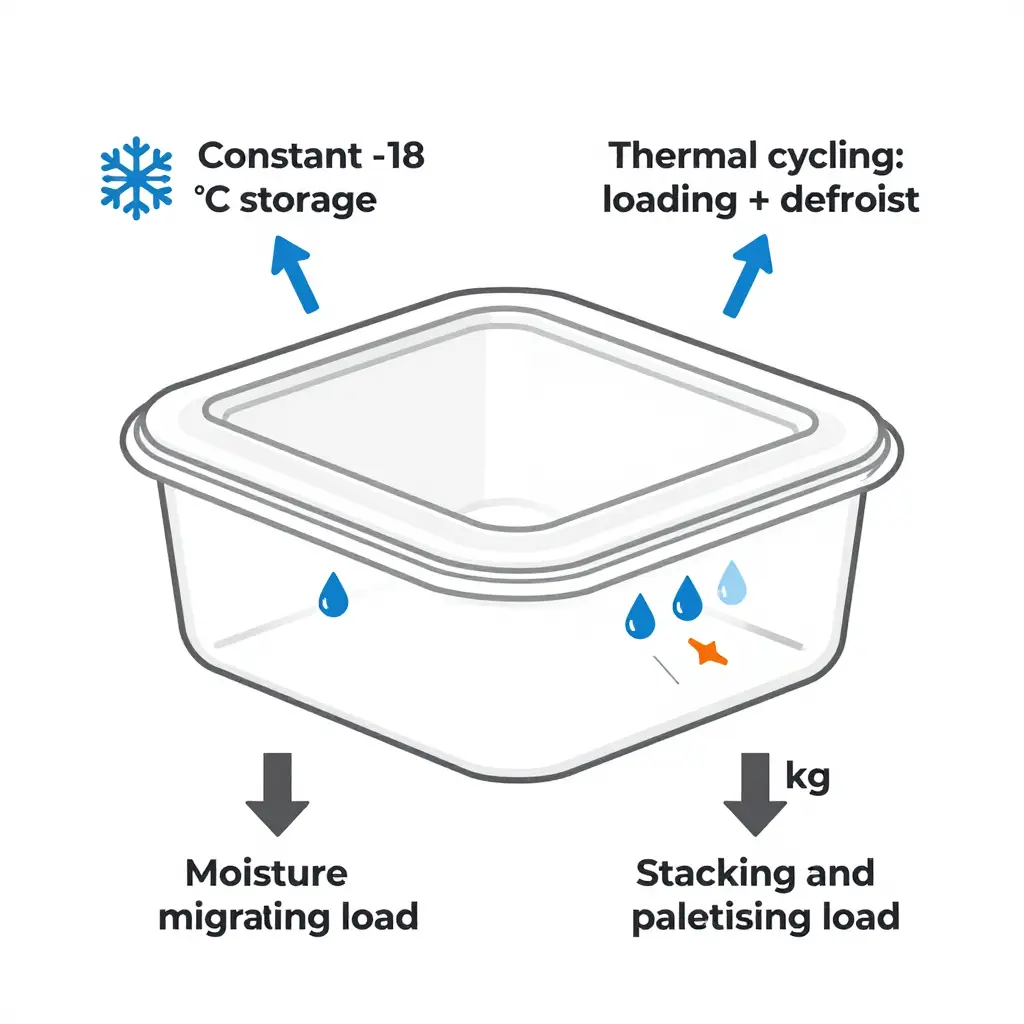
Four conditions overlap in a cold store, and every wall section has to tolerate all of them at once:
- Constant -18 °C storage. Product core and wall sit at the set point for months. A brittle material state stops being a transient and becomes the design condition.
- Thermal cycling during loading and defrost. Dock-side loading, door openings and coil defrost cycles push wall temperature up by several degrees and let it fall again, flexing the wall panel and the lid seam each time.
- Moisture migration. Free water leaves the food matrix, crosses the headspace and travels along the wall interface, then freezes and expands. Internal pressure rises, and ice keys into the lid seat.
- Mechanical impact loads. Stacking applies sustained compression; handling adds drop events that put their energy into corners, ribs and the base radius.
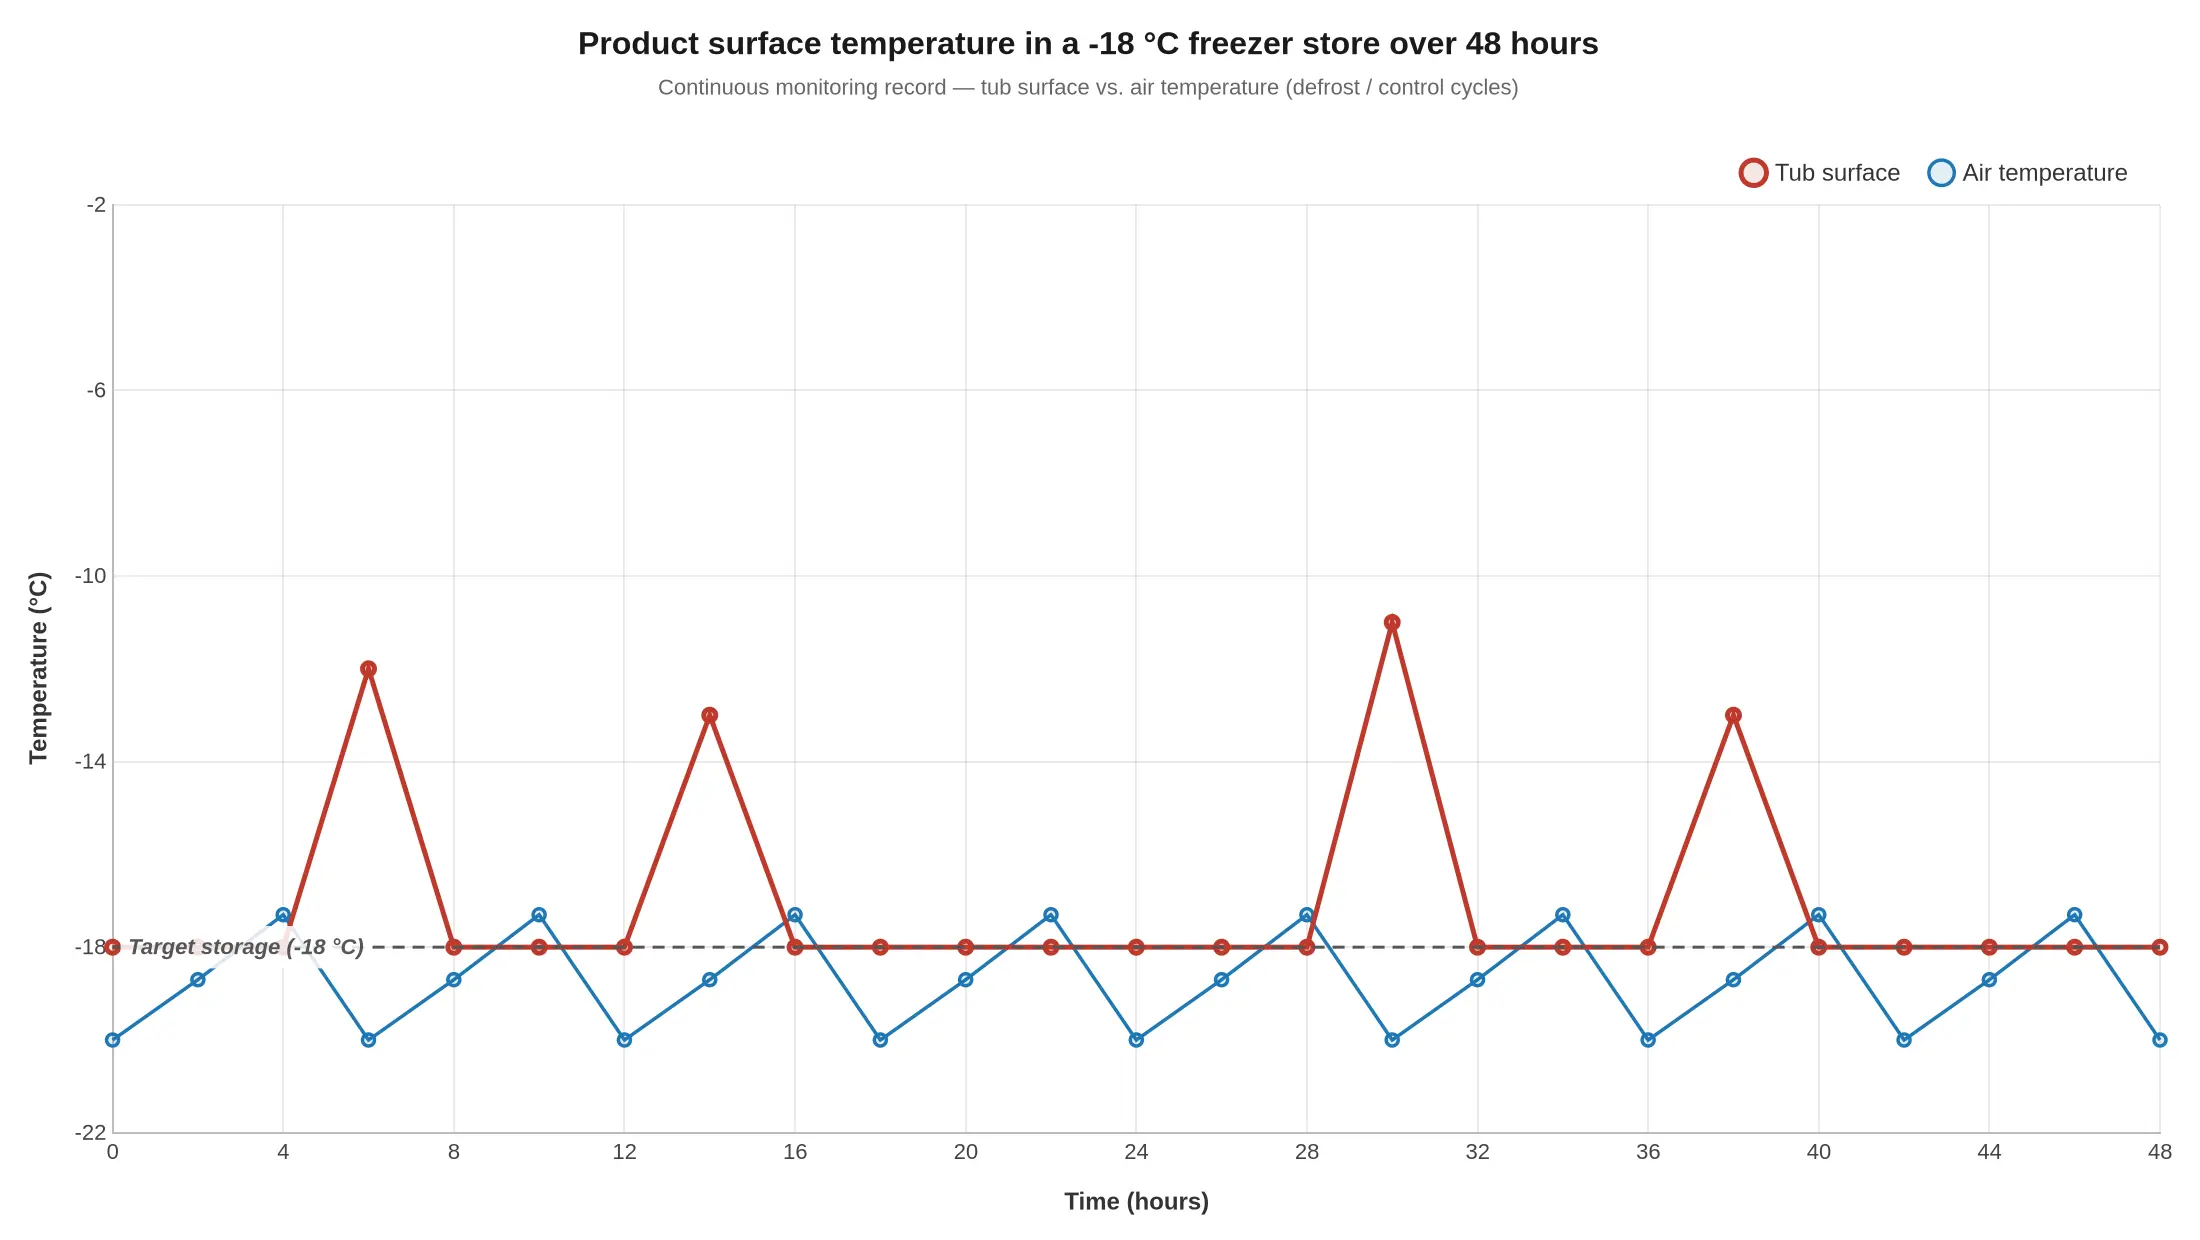
Figure 1: A nominal -18 °C set point still delivers repeated upward temperature excursions at the wall surface, so the wall has to be specified for cycling, not for a single constant value.
Five Material Concepts Behind These Failures
Glass transition temperature (Tg) marks where the amorphous phase stiffens and loses ductility. Crystallinity governs stiffness, barrier performance and mould shrinkage. Impact modification, usually an elastomer or rubber-phase dispersion, restores toughness below Tg. Low-temperature embrittlement is the loss of elongation that follows at -18 °C, and drop-test energy absorption measures how much impact a given wall section can take before a crack starts.
None of that is much use until it is mapped onto real geometry. Specifications written against rectangular tub formats and their wall sections show how minimum wall thickness and rib placement turn a resin datasheet into a container that survives the pallet, not just the freezer.
Polypropylene (PP) at -18 °C: Ductility, Crystallinity and the Role of Impact Copolymer
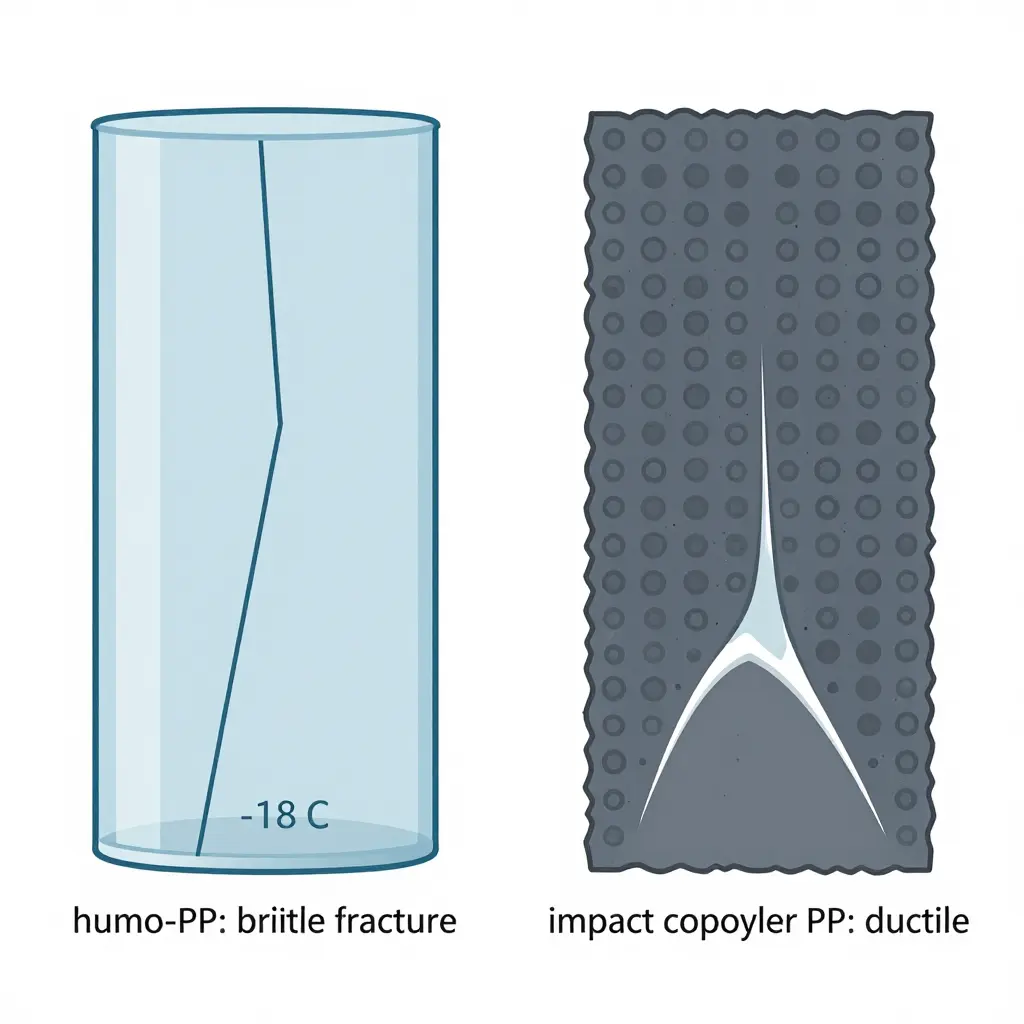
Polypropylene is a semicrystalline commodity polymer, with a density of 0.90-0.91 g/cm3 and a crystalline melting point of 160-170 °C. Those numbers set its thermal ceiling, not its low-temperature behaviour. Under freezer duty the controlling parameter is the glass transition of the amorphous fraction, which for PP homopolymer sits near 0 °C. At -18 °C that phase is glassy: segmental mobility is frozen out, the polymer can no longer shed energy by shear yielding, and it answers impact in a brittle, notch-sensitive way. A thin homopolymer wall gives a crack little volume in which to arrest, so a shoulder that takes a knock while frozen fractures instead of denting.
Impact copolymer PP fixes this by architecture rather than by plasticiser. An ethylene-propylene rubber (EPR) phase is polymerised into the matrix as micron-scale domains, and that separate low-Tg component stays mobile well below -18 °C. On impact the domains cavitate and trigger localised shear yielding in the surrounding matrix, so kinetic energy goes into deformation instead of a running crack. Ductility holds at -18 °C and, in higher rubber-content grades, at -30 °C and below.
Freezer specifications follow from that hierarchy. A freezer tub usually runs a nominal wall of 0.8-1.5 mm; thinner sections are dimensionally efficient but lose impact margin unless the resin is a copolymer grade. Service range is commonly quoted as -20 °C to 100 °C and above, which is why one resin spans blast freezing, hot fill and microwave reheating.
Three properties define PP’s place in frozen food packaging:
- Moisture barrier: low water-vapour transmission holds off desiccation, surface ice-crystal growth and freezer burn through long frozen storage.
- Thermal tolerance: a melting point of 160-170 °C and a service ceiling above 100 °C allow direct microwave reheating without visible distortion — a decisive advantage over PET tubs.
- Sealability and end-of-life: PP takes heat-sealable lid film with a compatible seal layer for leak-tight, tamper-evident closures, and carries resin identification code 5 for the PP recycling stream.
Neither trade-off is free. PP’s oxygen barrier is weaker than PET’s, so oxygen-sensitive lipids and pigments oxidise faster in frozen storage, and its semicrystalline morphology scatters light into haze, costing clarity against amorphous PET. For freezer tubs and lidded containers, toughness usually outweighs both; our PP food trays and containers show how a wall spec translates into real product geometry.
PP remains the default freezer material wherever mechanical toughness and reheating tolerance decide whether a container survives the cold chain.
PP vs PET at -18 °C: Material and Performance Comparison
Impact copolymer PP and PET (both A-PET and CPET grades) part company once the thermostat drops below zero. The table lines them up property by property against a -18 °C duty cycle. If you are already sizing tub formats, these rectangular freezer tub options show the geometries the wall-thickness figures apply to.
| Property | PP (impact copolymer) | PET (A-PET / CPET) |
|---|---|---|
| Glass transition temperature (Tg) | -10 to 0 °C (amorphous phase) | approx. 75-80 °C (same base resin for A-PET and CPET) |
| Melting point | 160-170 °C | 245-260 °C |
| Low-temperature impact behaviour at -18 °C | Ductile; rubber phase absorbs shock, dents instead of cracking | Brittle below Tg; A-PET crazes and cracks, CPET stiffer but still notch-sensitive |
| Clarity and transparency | Translucent to opaque, visible haze | High clarity (A-PET); opaque white (CPET) |
| Moisture vapour barrier | Excellent; WVTR approx. 0.2-0.5 g/m2/day at 25 µm | Moderate; WVTR approx. 1.5-3 g/m2/day at 25 µm |
| Oxygen / CO2 barrier | Moderate to low; OTR approx. 1500-2500 cc/m2/day/atm at 25 µm | Good; OTR approx. 50-100 cc/m2/day/atm at 25 µm |
| Microwave and oven tolerance | Microwave yes; no oven use, service limit approx. 100 °C | A-PET: microwave reheat only; CPET: microwave and dual-ovenable to 200-220 °C |
| Resin identification code | 5 (PP) | 1 (PET) |
| Typical nominal wall thickness, freezer tub | 0.8-1.5 mm (1.2 mm and up for drop-loaded duty) | 0.4-0.8 mm (A-PET); 1.0-2.0 mm (CPET) |
| Best-fit frozen-food application | Soups, stews, sauces, rice, bulk meal-prep and catering tubs | A-PET: cold-chain display and dry frozen items; CPET: dual-ovenable ready meals |
Values are typical ranges drawn from material data sheets and common moulded-part practice; confirm against your specific resin grade and mould design.
Where drop performance at -18 °C and moisture control decide the spec, PP wins on toughness per gram of wall. Where shelf clarity or oven transfer after thawing matters, PET is the better fit — A-PET for display, CPET for bakeable formats — provided the wall spec and corner radii account for brittle-fracture risk.
PET at -18 °C: Barrier Strength vs Low-Temperature Brittleness
“PET” is not one material in a freezer. The two grades that reach a cold store look identical on a shelf and behave nothing alike at -18 °C, and the difference comes from thermal history rather than chemistry.
A-PET: deep in the glassy state
Amorphous PET has a glass transition temperature (Tg) of roughly 78-80 °C. At -18 °C it sits about 95 °C below that, deep in the glassy state: stiff, strong in compression, with very little elongation before failure. Impact energy has nowhere to go, so a drop produces craze lines, stress whitening and fast crack propagation from corners, ribs and gate marks. This is textbook low-temperature brittleness, and thin sections with sharp internal radii make it worse.
CPET: crystallinity buys toughness in shape
CPET carries 30-40 % crystallinity from the thermoforming and heat-setting step. The crystalline domains act as a rigid scaffold: the tub holds dimensions through freeze-thaw cycling, resists creep in stacked pallets and tolerates oven reheating to around 200 °C. That is what makes genuine freezer-to-oven duty possible.
Wall specs and performance drivers
| Property | A-PET (amorphous) | CPET (crystallised) |
|---|---|---|
| Typical wall thickness | 0.4-0.8 mm | 1.0-2.0 mm |
| Crystallinity | < 5 % | 30-40 % |
| Service temperature | Chilled to frozen | Frozen to ~200 °C |
| Drop impact at -18 °C | Poor, shatters at corners | Good with adequate wall |
| Clarity | Excellent, glass-like | Opaque, white or pigmented |
| Barrier (O₂, aroma) | Excellent | Good to excellent |
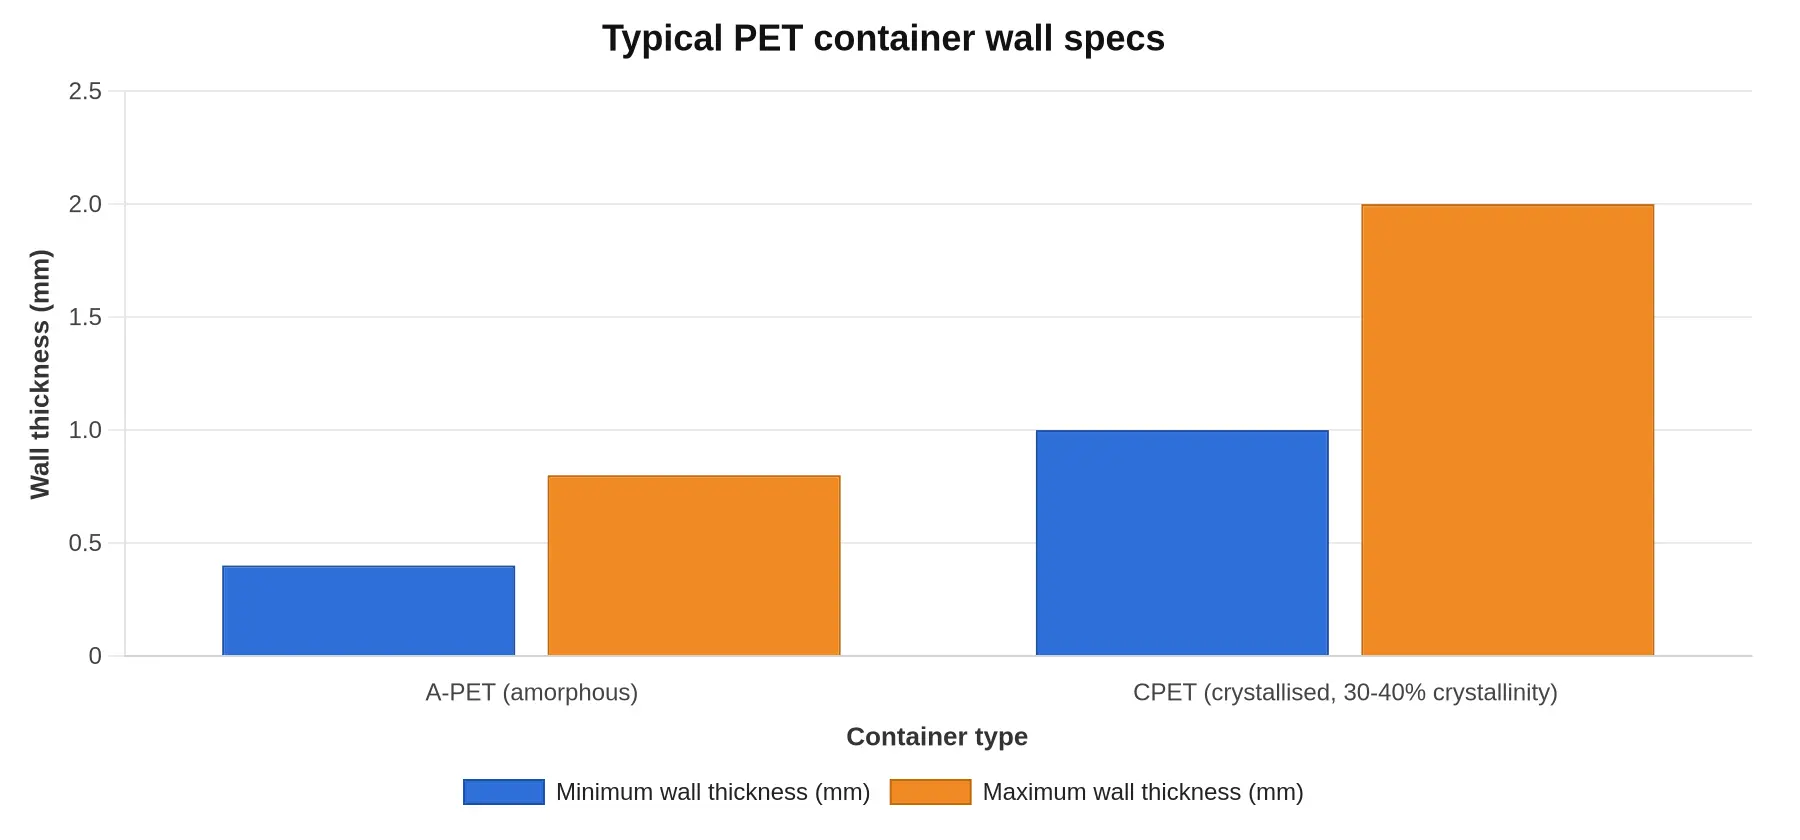
Both grades give PET containers an excellent oxygen barrier and strong aroma retention, which matters for oxidisable fats, fish, sauces and anything carrying citrus or spice volatiles. A-PET adds the optical clarity that sells product through a display lid.
What this means for frozen-food packaging specs
- A-PET is the right call for chilled display, dry-frozen goods and barrier-critical cold-chain storage where handling is controlled, cases are not drop-loaded, and the visual sell is the point.
- Freezer tubs that see real drop loads — retail multipacks, home delivery, food service — should specify CPET, or an impact-modified A-PET grade with elastomer or copolymer toughening, and be validated by a drop test run at -18 °C rather than at room temperature.
- Thin-wall A-PET carries the highest brittleness risk: below about 0.5 mm, with corner radii under 3 mm and unfilleted ribs, is where failures start.
The engineer’s one-sentence rule: Specify CPET or an impact-modified grade whenever a PET tub must survive a drop at -18 °C, and reserve thin-wall A-PET for barrier-critical, controlled-handling cold chain where clarity earns its place.
Wall Geometry: Where Cold Stress Actually Concentrates
Material grade gets most of the attention, but within a single PP or PET resin the geometry of the wall controls where frozen stress concentrates. The schematic isolates the three variables that matter most in a freezer tub: nominal wall section, vertical rib spacing, and the radius at the base transition.
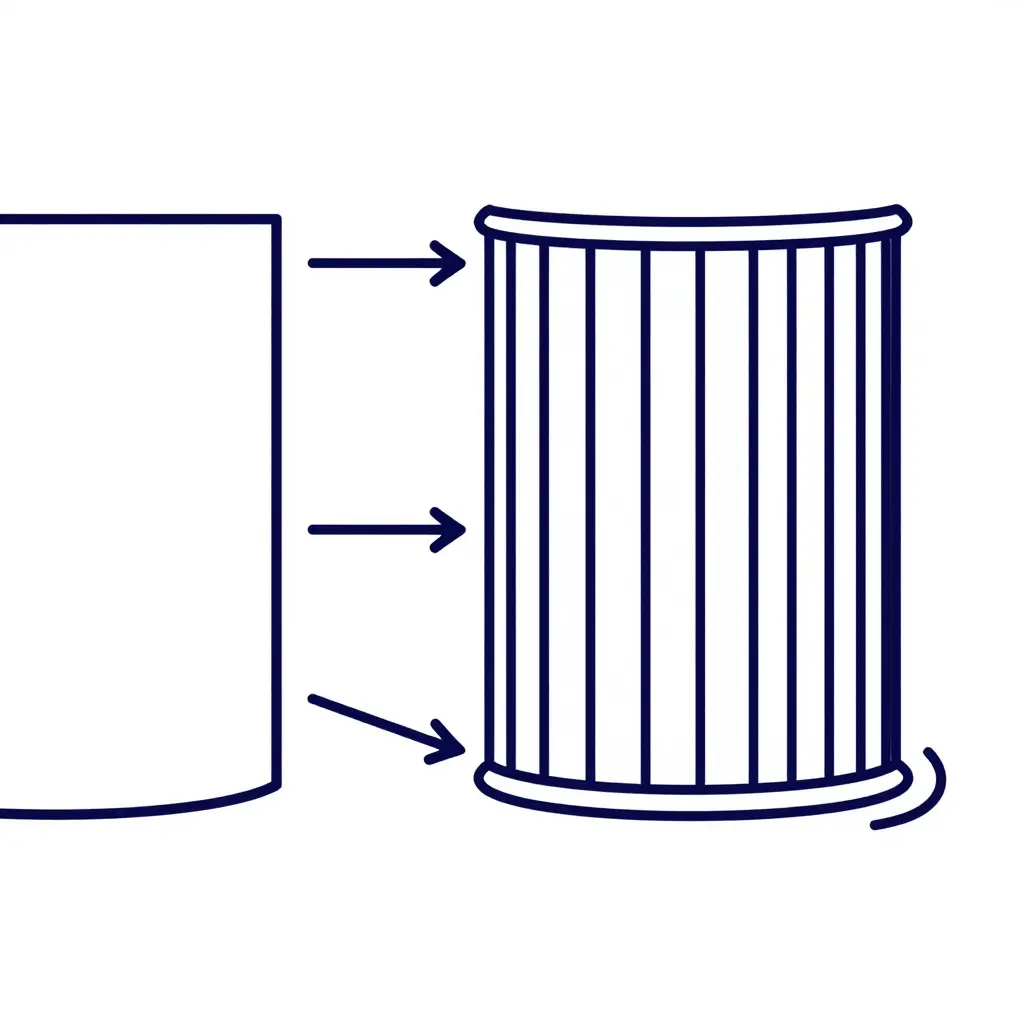
Figure 2: Side cross-section of two container walls. Left — thin, uniform section with a sharp 90-degree base corner and a step-change load path. Right — thicker section with evenly spaced vertical ribs and a rounded fillet at the base, letting the load path flow around the corner.
How to read the drawing
- Left wall, sharp corner. The load path meets an abrupt 90-degree transition and the arrows kink at the base. That kink stands in for a stress concentration point, where hoop and bending forces converge during ice expansion.
- Right wall, ribbed and radiused. Vertical ribs shorten the unsupported span of the wall; the fillet spreads the same load over a longer arc, so the arrows bend gradually instead of reflecting off a hard edge.
- Arrow direction only. Nothing in the drawing is to scale. It compares paths, not dimensions.
What it means for a wall specification
| Geometric feature | Thin wall, sharp corner | Thick wall, ribbed, radiused base |
|---|---|---|
| Wall section | Low bending stiffness | Higher bending stiffness per unit area |
| Rib layout | Unsupported span, higher deflection | Ribs break the span, reduced deflection |
| Base transition | Sharp 90-degree, stress concentration | Fillet radius, distributed load path |
| Likely failure mode | Corner cracking, base splits | Bulging or panel fatigue, rarely cracks |
Put this geometry review next to the resin choice and the specification will hold through repeated freeze-thaw cycles. Our ready-stock containers are a practical reference point for checking wall gauge and base design before you commit to a custom mould.
The Wall Spec That Decides Survival: Thickness, Rib Geometry and Corner Radius
A PP tub can pass every room-temperature check and still split on its first trip out of a -18 °C freezer. The resin grade is rarely the reason. The wall spec is: how thin the plastic actually gets in the places nobody measures, and how the geometry behaves once the polymer is frozen stiff.

Nominal thickness is a drawing value; minimum thickness is the real part
Nominal wall thickness is the target dimension on the 2D drawing, 1.2 mm for instance. It describes the mould cavity in its ideal state, and it is the number quoted in most purchasing conversations. It is not what ships.
Minimum wall thickness is the thinnest measured point on the moulded part, taken from a sectioned sample or a CT scan rather than from a single micrometer reading at a convenient spot. For a freezer-safe tub the minimum governs impact survival, because a frozen PP wall has almost no ductility left with which to redistribute stress. Failure starts at the thinnest section and propagates through it.
Why the gate end and the base transition decide the outcome
Two locations fail first, and neither is where the drawing dimension is easiest to hold.
- Gate end. Last region to fill, last to pack. Pressure has decayed along the flow path, the melt front is coolest, and shrinkage has already begun before holding pressure arrives. On a poorly balanced tool a 1.2 mm nominal wall commonly measures 1.02-1.10 mm here, which is why the spec needs a separate floor at this location.
- Base transition. The melt turns from a thin base into the sidewall. Shear peaks, the frozen skin forms early, and any sharp internal step creates a stress riser exactly where drop loads concentrate. A base corner that is thin and sharp is a guaranteed corner crack.
Tolerance bands worth writing into the spec
| Nominal wall thickness | Moulding tolerance | Minimum at gate end | Minimum at base transition |
|---|---|---|---|
| 0.8 mm | +/- 0.06 mm | 0.72 mm | 0.70 mm |
| 1.0 mm | +/- 0.08 mm | 0.90 mm | 0.86 mm |
| 1.2 mm | +/- 0.09 mm | 1.08 mm | 1.02 mm |
| 1.5 mm | +/- 0.10 mm | 1.35 mm | 1.28 mm |
Taper for demoulding and stacking. 1.0-1.5° per side on straight walls, 3-5° on textured surfaces. Too little draft forces ejection stress into the part at demould; too much eats nesting depth and destabilises palletised stacks.
Flange thickness and stiffness. The rim is the stiffest feature in the part and the first thing to take an edge drop. Run flanges at 1.6-2.0 mm, roughly 1.3-1.7 times a 1.2 mm sidewall, with a flat sealing land wide enough to take a lid skirt without overhang.
Rib pitch and depth. Rib thickness 0.5-0.6 of the wall, rib depth no more than 2.5-3 times the wall, pitch 2-3 times the wall thickness. Tighter pitch sinks the visible face; deeper ribs risk short fill and a weak root.
Base-to-wall radius. Keep the internal fillet at 3-5 mm and distribute material so the transition is thicker than the sidewall, never thinner.
Corner radius. 3 mm is the floor on any plan-view corner, and freezer duty wants more: 8 mm or above, opened further at the base. Below 3 mm, stress concentration in a frozen, notch-sensitive PP wall climbs sharply and corner drops fail predictably.
Verification method: the -18 °C drop test
No design should be accepted without a documented drop test. The method is fixed and repeatable:
| Orientation | Drop height | Drops per orientation | Conditioning before test |
|---|---|---|---|
| Corner | 1.2 m | 3 | 24 h at -18 °C |
| Edge | 1.2 m | 3 | 24 h at -18 °C |
| Base | 1.2 m | 3 | 24 h at -18 °C |
Each unit is filled to nominal capacity with a representative load, conditioned for 24 hours at -18 °C, and dropped onto a rigid concrete floor within 10 seconds of leaving the freezer. Pass criteria: no through-wall crack and no lid separation. Hairline whitening at a rib root is a flag, not an automatic fail, but it is worth recording.
Injection moulding variables that move the result
Gate location sets the flow length, and with it the pressure available at the gate end; a centre gate balances the fill but leaves the base rim as the last-to-pack zone. Packing pressure and hold time close the gap between nominal and minimum wall. Warpage control — cavity temperature symmetry and balanced cooling — keeps the base flat, so the tub sits square under impact. Melt flow index is a deliberate choice as well: a high-MFI PP fills thin sections easily and gives up impact strength at -18 °C, while a low-MFI grade survives the drop and asks for more injection pressure and a more generous wall spec.
If you are specifying containers alongside other packaging items, compare wall and rim conventions across the freezer-safe tubs and takeaway boxes range before locking a single tolerance band into the purchase order.
Quote the minimum wall, not the nominal. Mandate a 3 mm corner radius as the floor. Prove the spec with a 1.2 m, three-orientation, -18 °C drop test.
What Wall Thickness Actually Buys You
Before signing off on a tub spec, it helps to see what thickness buys. The chart plots low-temperature drop survival against nominal wall thickness for a PP impact copolymer under a realistic cold-chain condition: a 1.2 m drop from the freezer at -18 °C. Each bar is the mean of six representative sample lots per thickness, so it describes a test range rather than one supplier’s claim.
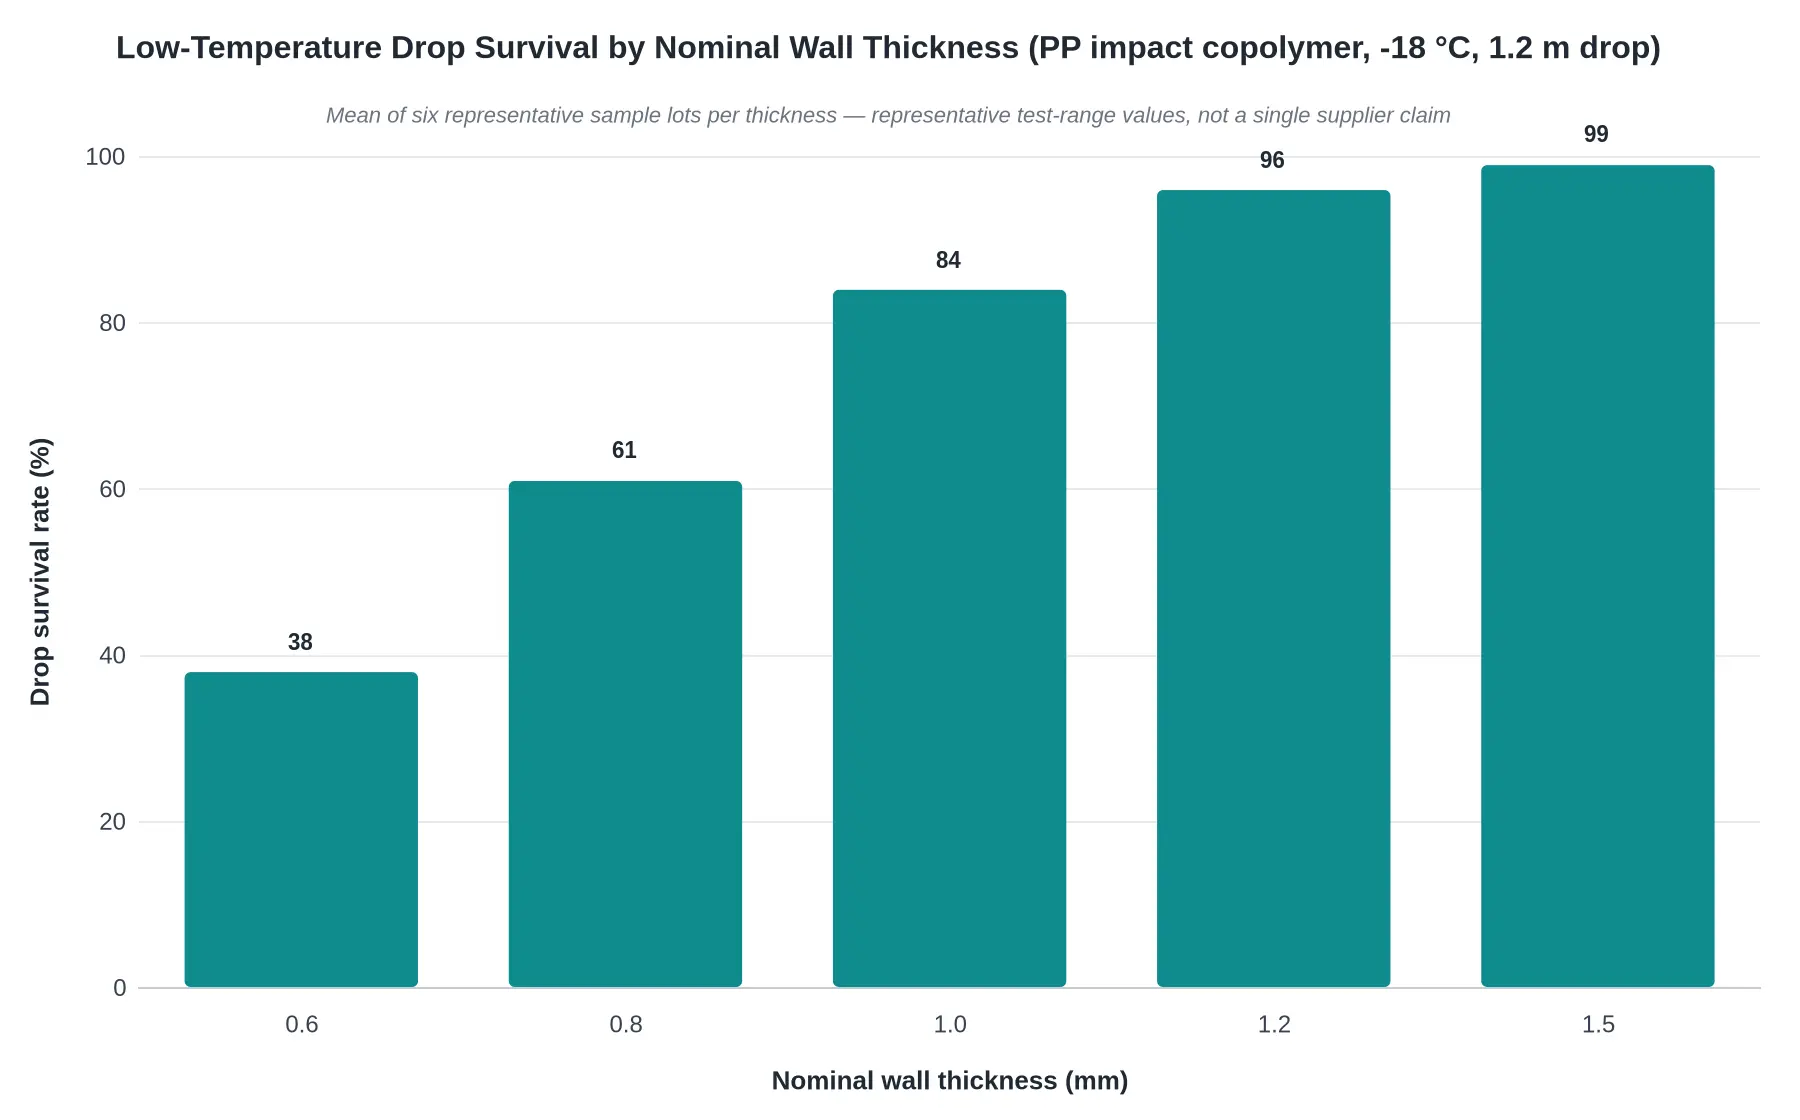
Figure 3: “Low-Temperature Drop Survival by Nominal Wall Thickness (PP impact copolymer, -18 °C, 1.2 m drop)”. Bars show the mean survival rate of six representative lots of PP impact copolymer dropped 1.2 m at -18 °C; values are representative test-range findings, not a single supplier’s specification. Read left to right to find where additional wall gauge stops improving survival.
Read it this way: the x-axis is nominal wall thickness in millimetres; the y-axis is the share of drops in which the container came through intact. The steep climb between 0.6 and 1.0 mm says the material is still brittle-dominated there. The flattening above 1.2 mm says the failure mode has shifted and extra grams of plastic stop earning their keep. Where the bars plateau is the practical design ceiling, not a marketing claim.
| Nominal wall thickness (mm) | Drop survival, six-lot mean (%) |
|---|---|
| 0.6 | 38 |
| 0.8 | 61 |
| 1.0 | 84 |
| 1.2 | 96 |
| 1.5 | 99 |
In practice, 1.0 mm is where a PP impact copolymer starts behaving like a freezer container rather than a takeaway tub, and 1.2 mm is the usual sweet spot for repeated handling in catering and food-service logistics. Where freezing is paired with stacked transport, specify thickness and container format together — rectangular bowls with a defined wall spec, for instance, so that geometry and gauge are validated as one system instead of bolted together later.
Chart.js Configuration
// Requires chartjs-plugin-datalabels for the on-bar percentage labels
const dropSurvivalByThickness = {
  type: 'bar',
  data: {
    labels: ['0.6', '0.8', '1.0', '1.2', '1.5'],
    datasets: [{
      label: 'Drop survival rate',
      data: [38, 61, 84, 96, 99],
      backgroundColor: '#0F8B8D',
      borderColor: '#0F8B8D',
      borderWidth: 0
    }]
  },
  options: {
    responsive: true,
    maintainAspectRatio: false,
    layout: { padding: { top: 8, right: 20, bottom: 8, left: 8 } },
    plugins: {
      legend: { display: false }, // legend off: single series
      title: {
        display: true,
        text: 'Low-Temperature Drop Survival by Nominal Wall Thickness (PP impact copolymer, -18 \u00b0C, 1.2 m drop)',
        color: '#1F2933',
        font: { size: 16, weight: '600' },
        padding: { top: 6, bottom: 18 }
      },
      subtitle: {
        display: true,
        text: 'Mean of six representative sample lots per thickness \u2014 representative test-range values, not a single supplier claim',
        color: '#6B7280',
        font: { size: 11, style: 'italic' },
        padding: { bottom: 14 }
      },
      datalabels: {
        anchor: 'end',
        align: 'top',
        offset: 4,
        color: '#1F2933',
        font: { size: 12, weight: '600' },
        formatter: (value) => value + '%'
      }
    },
    scales: {
      x: {
        title: {
          display: true,
          text: 'Nominal wall thickness (mm)',
          color: '#1F2933',
          font: { size: 13, weight: '600' },
          padding: { top: 10 }
        },
        grid: { display: false, color: '#D7DBDF' },
        border: { color: '#C7CCD1' },
        ticks: { color: '#374151', font: { size: 12 } }
      },
      y: {
        min: 0,
        max: 100,
        title: {
          display: true,
          text: 'Drop survival rate (%)',
          color: '#1F2933',
          font: { size: 13, weight: '600' },
          padding: { bottom: 10 }
        },
        grid: { display: true, drawTicks: false, color: '#E8EAED', lineWidth: 1 },
        border: { display: false },
        ticks: { color: '#374151', font: { size: 12 }, stepSize: 20, padding: 6 }
      }
    },
    elements: {
      bar: { borderRadius: 3, borderSkipped: false, categoryPercentage: 0.62, barPercentage: 0.9 }
    }
  }
};

// chart.js
// const ctx = document.getElementById('dropSurvivalChart');
// new Chart(ctx, dropSurvivalByThickness);
Freezer Tub Wall Specification Checklist
Each line below is one measurable acceptance point for a PP or PET tub rated to -18 °C. Paste them straight into the purchase document.
- Nominal sidewall thickness: 1.2 mm for PP; 1.0 mm for CPET or 0.9 mm for impact-modified A-PET; absolute permitted minimum 1.0 mm at any measured point on a PP tub.
- Thickness tolerance band: ±0.08 mm over any 100 mm span, verified at six points per sidewall.
- Rib pitch and depth: pitch 12-15 mm, rib depth-to-wall ratio 1.5:1, ribs terminating 10 mm below the flange.
- Plan corner radius: 8 mm minimum internal, opened to 12 mm at base corners to spread impact stress.
- Base-to-wall transition radius: 3 mm minimum, fully blended — no sharp step or knife edge permitted.
- Flange thickness and stiffness: 1.8 mm minimum, deflection ≤2 mm under a 10 N mid-span load.
- Resin grade and melt flow index: virgin PP copolymer at MFI 8-12 g/10 min (230 °C/2.16 kg); PET at 0.80-0.85 dL/g IV.
- Impact modifier content: 5-10% ethylene-propylene elastomer in PP, confirmed by FTIR against the approved reference sample.
- Drop test at -18 °C: 5 of 5 filled tubs conditioned 24 h, dropped 1.2 m onto concrete, no crack, split or lid release.
- Declared service temperature range: -20 °C to +95 °C continuous, with -30 °C allowed for short-term excursions only.
- Lid fit and sealing integrity: removal force 15-30 N; zero leakage after a 30 s inverted hold at -18 °C.
- Static stack load capacity: 25 kg on the lidded tub for 24 h at -18 °C, permanent deformation ≤2 mm.
Attach this sheet to the tub drawing, and cross-check the formats against our freezer-ready container stock before the PO is released.
Spec-Driven Selection: Choosing PP or PET for a Frozen-Food Packaging Program
For a frozen-food program, the PP vs PET question is not a matter of preference but of thermal and mechanical duty. PP (polypropylene) keeps useful toughness at -18 °C and tolerates reheating. PET (polyethylene terephthalate) brings clarity and stiffness, then turns brittle as it approaches deep-freeze temperatures and softens well below microwave duty.
Freezer storage with microwave reheating. Specify PP, with a homopolymer or copolymer grade whose low-temperature impact performance is documented, and a wall spec thick enough to survive repeated cycling from -18 °C to above 100 °C without stress whitening, rim warping or lid-seat distortion. Ask for written confirmation that the grade is microwave-suitable and that no additive migrates at reheating temperatures.
Freezer plus oven dual use. Specify PP only where the resin data sheet states an oven service temperature ceiling and the program formally accepts that ceiling. A freezer-safe container is not automatically oven-safe, so do not approve the duty on that assumption. Procurement should hold written ratings for both ends of the cycle, plus a lid that is removed before heating or separately rated.
Chilled or cold display with high barrier needs. Specify PET, or a PP/EVOH structure where barrier and toughness both have to hold. Clarity, print quality and oxygen barrier outweigh low-temperature impact here, and the -18 °C rule does not govern because the product never reaches deep-freeze.
Translating the rules into a written purchase specification
Five clauses carry the decision.
- Material grade: resin family, copolymer type, MFI range, food-contact declaration and the exact grade designation, stated so that any substitution requires written approval.
- Wall spec: nominal wall in millimetres with a defined measuring datum, minimum wall at corners and base radius, rim thickness, and permitted thickness variation across the part.
- Drop test method and acceptance criteria: conditioning at -18 °C for a stated dwell, a defined drop height and surface, a defined set of orientations, and zero leakage and zero cracking across the sample, with lid retention recorded separately.
- Dimensional tolerances: top-out diameter, depth, capacity to fill line, stacking height and lid interference fit, each with a tolerance band and a stated gauge method.
- Lot sampling: the AQL plan, sample size per lot, inspection level and the inspection record retained per shipment.
Qualify before committing volume
Before releasing a volume order, require production-intent samples tested at -18 °C: same tool, same resin grade, same wall spec as serial production, not an ambient-temperature trial. Samples from a different grade or from a pre-production tool prove nothing about the delivered part. Then write the re-qualification trigger into the specification itself. Any change of resin grade or resin supplier, any change to the wall spec beyond the stated tolerance band, and any tool modification affecting cavity geometry void the previous approval and require a fresh freeze-drop and dimensional qualification. For programs pairing a rectangular footprint with freezer duty, our rectangular bowls and containers are a practical starting point for gauge and format review.
Aligning Freezer Tubs with the Rest of the Packaging Line
A freezer tub specification does not stand alone. The same cold-chain profile applies to the meal and bento boxes that carry the defrosted or reconstituted product, the trays and plates used for service presentation, and the bowls, lids and cup accessories that complete the pack. Thermal and moisture performance therefore has to hold component to component. If the tub wall resists condensation at -18 °C while a lid, tray or secondary box does not, moisture migrates to the weakest interface, stack strength shifts under load, and handling behaviour changes between the primary container and its outer packaging. Review grade, wall thickness and barrier character as one system rather than as separate line items, so that dimensional stability, seal integrity and load-bearing capacity hold at the same rate across every element of the pack.
FAQ: Freezer-Safe Plastic Containers
Is PET freezer-safe at -18 °C?
Crystallised PET (CPET) grades are rated for -18 °C service. Standard amorphous APET sits far below its glass transition at that temperature and loses impact strength, so it needs impact modifiers, a 1.0 mm minimum wall and generous corner radii to survive handling.
What wall thickness is required for a 1 litre freezer tub at -18 °C?
Specify 1.2-1.5 mm sidewalls and a 1.5-2.0 mm base for PP; 0.8 mm sections lose too many drops to be worth the resin saving. Verify with 24-hour -18 °C conditioning followed by a 1.2 m drop test per ASTM D5276.
Why do tubs typically crack at the corner or base transition?
Those zones concentrate stress. Sharp internal radii raise the stress concentration factor, moulded-in residual stress peaks there, and water in food expands about 9% on freezing, so the base-to-wall junction is loaded again on every drop and handling event.
Can PP freezer tubs go from the freezer directly to the microwave?
Yes. PP homopolymer tolerates temperatures up to roughly 100 °C, so -18 °C to microwave sits inside its range, but direct full-power heating creates thermal shock that warps lids. Vent the closure and heat on medium power in short intervals.
Does clarity change after long storage at -18 °C?
APET clarity holds at -18 °C because the polymer is below its glass transition, where chain mobility is frozen and crystallisation cannot progress. Stressed corners can still develop haze and stress whitening over months. PP stays translucent regardless of grade. Confirm haze with a hazemeter per ASTM D1003 after 90-day storage.
For production-ready containers in these gauges, review our freezer-capable in-stock box formats.
Conclusion: Match the Polymer to the Temperature and the Wall Spec to the Load
-18 °C is an active stressor, not a storage condition. Cold pushes a polymer toward its brittle range, and the PP vs PET split widens exactly there: one resin keeps usable impact resistance, the other trades toughness for stiffness. A specification written without that temperature shift in mind is written for the wrong conditions.
Grade and wall geometry govern survival together. A well-chosen resin in an under-specified wall still fails at corner radii, base fillets and lid-seat rims, because those are the points where stress concentrates during a cold impact. A generous wall in the wrong grade cracks just as reliably. Real drop performance is the product of both decisions, which is why sourcing on resin name alone, or on wall thickness alone, keeps producing failures in the field. Buyers comparing freezer-safe container stock should read grade and geometry as one package, not two line items.
The practical conclusion is narrow: a written wall spec plus a defined -18 °C drop test is the only acceptance criterion that can be audited. The spec states resin grade, nominal thickness with tolerance, and the geometry held at stress points. The test states conditioning time, drop height, orientations and pass criteria. Anything short of that, including a generic “freezer safe” claim, predicts nothing about cold-chain performance. Put both documents into the purchase order and the incoming inspection sheet before the next container run is released.